
 HOTLINE:+8613974960765 +8618507312158 HOTLINE:+8613974960765 +8618507312158


— Knowledge —
— PRODUCTS —
 Service Hotline +8613974960765
Email:susie@hnljpump.com
Mobile:+8618507312158
TEL:+8613974960765
Right Angle Gearboxes
Publication date:2025/2/25 23:40:30 popularity: [content:visits]
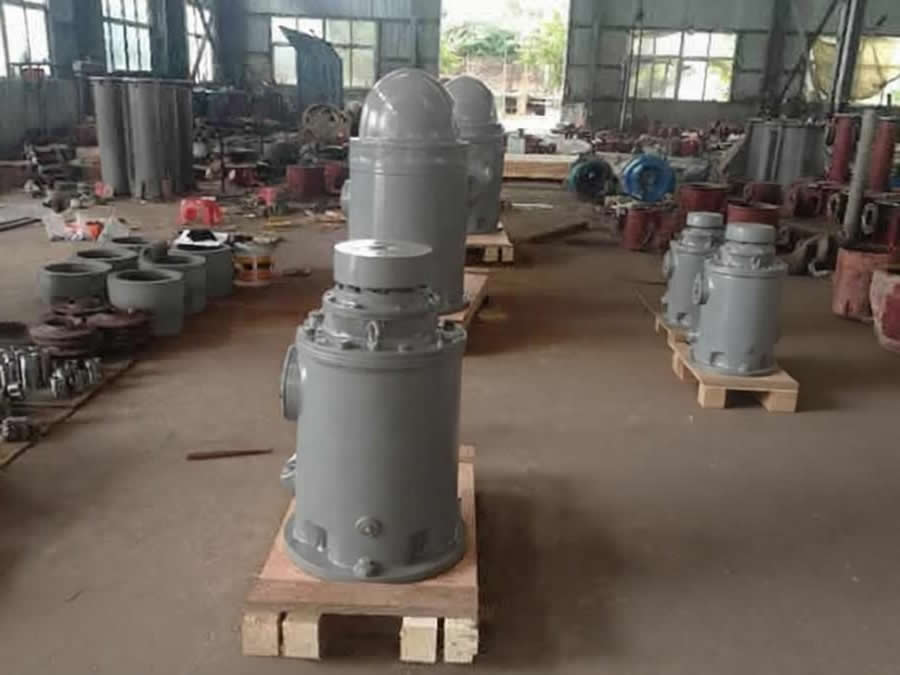
This case study focuses on the renovation project of a long-distance concentrate conveying system in a large metal beneficiation plant. The heavy load anti-wear H-series right angle gearbox is used to drive the slurry pump, which solves the core pain points of traditional direct drive in high slag content, strong abrasion, alternating impact conditions, such as limited space, rapid component wear, and axial thrust overload. The slurry conveying system can operate continuously and stably for a long time, avoiding significant losses caused by the complete shutdown of the beneficiation production line due to conveying interruption.
⛏️ Project background and original pain points
The beneficiation plant has an annual processing capacity of 3 million tons of ore. The designed flow rate of the concentrate slurry conveying system is 800m ³/h, with a head of 120m. The solid particles in the slurry account for 40% and contain a large amount of high hardness metal slag particles. The original system used a conventional motor-driven slurry pump scheme, which exposed multiple serious problems during operation:
The spatial layout is severely limited: the height of the pump room in the main building of the beneficiation plant is only 3.5m, and the vertical motor is directly stacked above the slurry pump body. The total axial height of the unit exceeds 3.2m, and there is insufficient space for daily operation and maintenance of the crane. When disassembling the pump body and replacing the overcurrent components, it is necessary to temporarily remove the pipelines and bridge facilities at the top of the pump room. A single maintenance takes more than 72 hours, and the beneficiation production line is forced to shut down completely, resulting in a loss of over one million yuan per shutdown.
Frequent occurrence of strong abrasion impact overload: High hardness slag particles in the slurry can cause severe fluctuations in the axial thrust of the pump operation, with a fluctuation amplitude of up to 70%. The original vertical motor has a rated bearing capacity of only 75000N, which is affected by alternating impact loads for a long time. On average, bearing burnout faults occur within 5 months, and the unplanned failure rate of the slurry conveying system is as high as 25%, seriously affecting the continuity of mineral processing production.
Rapid wear and tear in dusty slurry environments: The air in the beneficiation workshop is filled with a large amount of mineral dust particles, and there is a small amount of slurry splashing at the pump shaft seal. The sealing protection level of ordinary gearboxes is insufficient, and mineral dust and slurry are prone to invade the interior, causing rapid abrasive wear on the gear meshing surface. On average, tooth surface pitting and vibration exceeding the standard faults occur within 9 months, and the equipment operation and maintenance cost is more than 5 times that of ordinary clean water pumps.
High energy consumption: The original direct drive scheme cannot flexibly adjust the output speed of the pump, and can only control the slurry conveying flow through the outlet valve throttling, resulting in a large amount of energy being wasted. The annual power consumption of a single slurry pump exceeds 5.2 million kWh, and the system's operating energy consumption far exceeds the industry average level.
🛠️ Customized selection scheme for H-series right angle gearbox
For the special working conditions of high abrasion and strong impact in the slurry transportation of the beneficiation plant, the heavy-duty anti-wear upgraded H-series right angle gearbox is selected, and the core configuration is fully adapted to the strict requirements of the beneficiation scene:
Accurate matching of core parameters:
Suitable for a horizontal motor with an input power of 1250HP (approximately 932kW), with 30% power redundancy reserved. The rated input speed is 1500rpm, and the pump output speed is 1875rpm through a customized transmission ratio of 1.25:1, fully matching the operating point of the slurry pump with a rated flow rate of 800m ³/h and a head of 120m.
Upgraded heavy-duty thrust roller bearings with a rated axial thrust bearing capacity of 125000N, fully covering the maximum instantaneous axial thrust of 110000N under slurry impact, and reserving 13% thrust redundancy to completely solve the bearing overload problem caused by alternating axial impact loads.
Special optimization of mineral processing conditions:
The gears are treated with 20CrMnTi alloy steel carburizing and quenching, with a tooth surface hardness of HRC60 or higher. Combined with a 6-level precision grinding process, the anti-wear ability is more than twice that of ordinary gears, which can resist slight wear caused by mineral dust intrusion and extend the service life of the gears.
The shaft end adopts a multiple dust-proof and waterproof sealing structure, with a protection level upgraded to IP66, completely blocking the intrusion of mineral dust particles and splashing slurry into the gearbox, preventing impurities from entering the lubricating oil and causing tooth wear and tear faults, and adapting to the special environment of high dust and multiple abrasive media in the beneficiation workshop.
Layout and operation adaptation optimization:
The horizontal motor is horizontally arranged in the safe area on the ground of the pump room. It drives the vertical slurry pump vertically after turning 90 degrees through the H-series right angle gearbox. The total axial height of the unit is reduced from 3.2m to 1.8m, perfectly adapting to the narrow vertical space of the pump room. There is no need to modify the original pump room steel structure, greatly reducing the construction cost of the modification.
Equipped with independent forced oil injection lubrication and external cooling system, the oil temperature can be stably controlled below 55 ℃. At the same time, an online oil monitoring sensor is installed to detect the content of metal abrasive particles in the lubricating oil in real time, predict the wear status of gears and bearings in advance, and avoid sudden failure during unmanned periods.
✅ Actual testing effect of project implementation
After the renovation project was put into operation, it has been running continuously for 36 months without major faults, and its performance indicators far exceed the production standards of the mineral processing industry
Significant improvement in reliability: The heavy-duty thrust bearing of the gearbox fully supports all the alternating axial loads of the pump, and the vibration value of the shaft system remains stable below 3.0mm/s, completely eliminating the original motor thrust bearing burnout fault. The continuous fault free operation time of the equipment has been extended from 5 months to 36 months, and the reliability of the slurry transportation system has been improved to 99.9%, completely avoiding the loss of production stoppage caused by transportation interruption.
Significant energy-saving benefits: By accurately matching the transmission ratio of the gearbox and eliminating the throttling adjustment of the original outlet valve, the overall transmission efficiency of the system has been improved to 97%. A single slurry pump can save 3.5 million kWh of electricity annually. Calculated at an industrial electricity price of 0.7 yuan/kWh for the beneficiation plant, the annual direct increase in revenue exceeds 2.45 million yuan, and the entire renovation cost can be recovered in 10 months.
The anti-wear performance has been greatly enhanced: IP66 level multiple dust-proof seals completely block the intrusion of mineral dust and slurry, and the cleanliness of the lubricating oil inside the gearbox remains within NAS8 level for a long time. The gear wear is only 40% of the industry average level, and the equipment lubricating oil replacement cycle has been extended from 2 months to 18 months, reducing annual operation and maintenance costs by 80%.
Significant improvement in operation and maintenance efficiency: After the total height of the unit was significantly reduced, daily maintenance operations for replacing pump overcurrent components can be directly carried out using conventional on-site cranes for lifting. The single disassembly and maintenance time has been reduced from 72 hours to 6 hours, and the downtime for maintenance of the mineral processing production line has been reduced by 90%, greatly improving the effective production time throughout the year.
📌 Summary of core project experience
When selecting the slurry transportation scenario for the beneficiation plant, it is necessary to choose customized H-series models with high thrust bearing capacity, reserve more than 30% power redundancy, and increase the operating coefficient KA value to 2.5 to resist the strong alternating impact load caused by high slag slurry. It is prohibited to directly use standard models for ordinary clean water pumps.
In the environment of high dust and multiple abrasive media in the beneficiation workshop, the protection level must be upgraded to IP66, equipped with multiple dust-proof and waterproof sealing structures to avoid the intrusion of mineral dust and slurry into the interior, which can cause abrasive wear on the tooth surface. This is the core key to extending the service life of the equipment.
The H-series right angle gearbox solution can be directly replicated and promoted to various high abrasion and strong impact mining conveying scenarios such as slurry conveying in metal beneficiation plants, tailings conveying, and coal slurry conveying in coal washing plants. It is currently the mainstream technology route in the beneficiation industry to improve production continuity, reduce costs and increase efficiency.
Previous:Case analysis of H-series right angle gearbox in coal mine drainage system
Next:What is the energy-saving effect of the H series right angle gearbox in power plant renovation?
Related Recommendations

Service hotline
screenshots ,WeChat Scan the Qr Code
WeChat:ljpump6666